Tuesday, July 19, 2016

Rim Speed Limits For Sheaves / Pulleys / Sprockets

Belt drive hardware has rotational speed limits in order to prevent excessive hoop stress levels that could result in physical material failures.  Material failures can be catastrophic with fragments thrown outward at high velocities and energy levels, so speed limits should not be exceeded.

Speed limits are based on the hardware material, as well as on the hardware configuration.  Block style hardware is inherently stronger than hardware with rims or spokes, so can operate at higher speeds.

Rotational speed limits are most commonly expressed in terms of rim speeds.  Common units used to express rim speed are feet per minute (ft/min) and meters per second (m/s).  Maximum rpm limits can be calculated from rim speeds with hardware diameters known.  An equation to calculate hardware rpm from rim speed is as follows:

RPM = (Rim Speed (ft/min) x 3.82)/Diameter (in)

A table from the Mechanical Power Transmission Association Standard B13i-2013 containing rim speed limits for a variety of hardware configurations and materials is as follows:


Belt drive hardware is often stamped with maximum rpm values, and will likely be based on this data.

If you have any questions, feel free to contact Gates Product Application Engineering at ptpasupport@gates.com or at 303.744.5800.

Tuesday, July 12, 2016

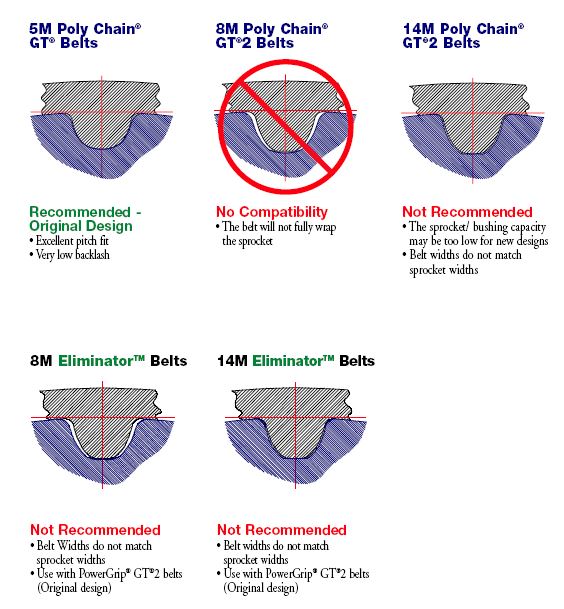
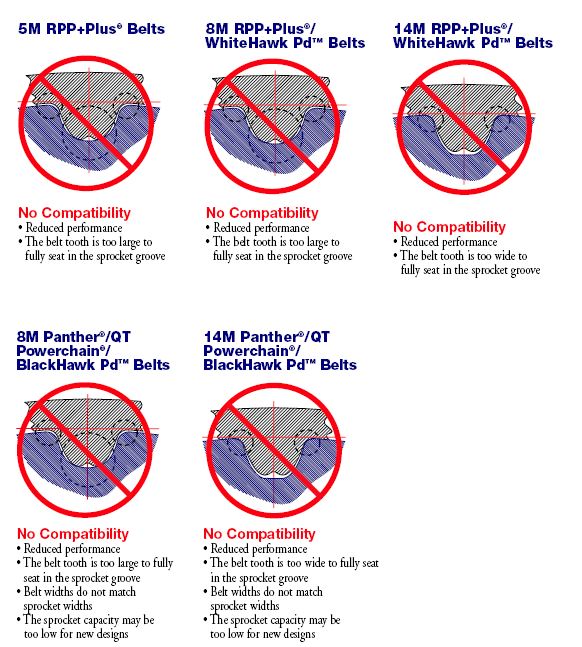
Will It Fit - Poly Chain GT2 Sprockets

What belt will fit into what industry standard sprocket is a question we regularly receive here in Product Application.  Below is information regarding what Gates belts will fit into standard Poly Chain GT2 sprockets.  

**When designing belt drives for NEW APPLICATIONS with Poly Chain GT Carbon power ratings: DO NOT use Poly Chain GT sprocket systems.  Poly Chain GT sprockets/bushings may not handle the increased torque load capacity and damage to the sprocket and/or bushing may occur.  ONLY use Poly Chain GT2 sprockets for new designs.** 


For any additional questions, feel free to contact us at PTPASupport@gates.com or 303-744-5800.

Tuesday, June 21, 2016

Understanding V-belt Construction Terms

V-belt construction features can be described by a variety of terms, which can cause confusion.  Here are some of the most common terms you may encounter:

  • Banded:
    • A fabric layer surrounds the belt
    • Also referred to as wrapped or covered
  • Bareback:
    • A type of banded V-belt where the fabric is not impregnated with rubber
    • Also referred to as low friction, dry cover, or clutching cover
  • Bandless:
    • No fabric surrounding the belt
    • Also referred to as cut edge, raw edge, or machined edge
  • Notched:
    • The bottom of the belt is notched (not flat)
    • Also referred to as cogged, molded notch, or cut notch
  • PowerBand®:
    • Multiple V-belt strands joined with a common backing
    • Also referred to as joined


Wednesday, June 8, 2016

Interchanging OEM Original Equipment V-belts With Standard Aftermarket V-belts

V-belts are commonly used in many light duty type applications including outdoor power equipment (lawn mowers, rotor tillers, snow blowers, etc.), light duty ventilation fans, power tools (table saws, drill presses, wood lathes, etc.) and much more.  V-belts eventually need to be replaced, and obtaining appropriate replacements can be challenging.

OEM Originals
Replacement belts can nearly always be obtained from the original equipment manufacturers, and this is usually the best practice.  OEM Manufacturers often use belts that have been custom manufactured for them in special constructions or in custom lengths that function best in their equipment.  These special constructions are proprietary, so the special features may not be easily determined.

Truflex and PowerRated Replacements
If original OEM V-belts cannot be obtained, replacement belts can sometimes be identified dimensionally although performance and functionality may not be the same as the OEM originals.  When considering replacement belts from our Truflex and PowerRated light duty V-belt product lines, there are additional considerations.

Clutching Applications
Some applications use belts to provide a clutching function to engage and disengage the equipment.  Only PowerRated type V-belts should be used in these applications as they have been designed with a bareback type cover that allows graceful slippage and aramid tensile cords that will not shrink like Truflex V-belts when hot from slippage.  Using conventional Truflex V-belts could cause unsafe machinery engagement and belt shrinkage could prevent disengagement, resulting in potentially hazardous circumstances.

V-belt Length Variations
Standard Truflex and PowerRated V-belts may not fit applications like OEM originals.  Standard V-belts may be too short to easily install or too long, resulting in adjustment pulleys moving to the end of their travel and not able to apply sufficient belt installation tension.  The position of spring loaded tensioning pulleys may also change, resulting in an increase of decrease in the proper belt tension.

PowerRated For Increased Robustness
Identically sized PowerRated V-belts can sometimes be used in place of Truflex V-belts for added load capacity and robustness.  This can sometimes improve belt service life when Truflex V-belt performance is less than desired.  Truflex V-belts should generally not be substituted for PowerRated V-belts, though.

Interchanging with Industrial V-belts
Identically sized Industrial A-Section and B-Section V-belts can sometimes be used in place of Truflex V-belts for added load capacity and durability.  Note, however, that small sheave diameters often used in these applications may be too small for solid banded A-Section and B-Section V-belts.  AX-Section and BX-Section (notched) V-belts are more flexible and tolerant of small sheave diameters, so may perform better.

Summary
Identifying correct replacement belts for equipment can be challenging.  We recommend that you consult original equipment manufacturers first for the best replacement.  Then consider the functionality needed by the belt in selecting V-belts from our standard product lines.  Contact Gates Product Application Engineering for further information at 303.744.5800 or ptpasupport@gates.com.

Tuesday, May 31, 2016

Will It Fit - GT2 Sprockets

What belt will fit into what industry standard sprocket is a question we regularly receive here in Product Application Engineering.  Below is information regarding what Gates belts will fit into standard PowerGrip GT2 sprockets.  


For any additional questions feel free to look through our other blog topics or contact us at ptpasupport@gates.com or 303-744-5800.


Minimizing V-belt Drive Noise

To minimize the noise level of your V-belt drive, pay close attention to tension and alignment.

Improper V-belt tension can cause the belt to slip and squeal. Misalignment creates interference at the belt’s entry point into the sheave, resulting in a louder drive.

Information on proper belt installation tension and alignment is detailed in the V-belt manual:

HEAVY-DUTY V-BELT DRIVE DESIGN MANUAL


Wednesday, May 4, 2016

Hose Cleanliness


Hose Cleanliness

When the customer becomes more dependent on ISO standards, your
strategy needs to reflect a dedication to system cleanliness.

What is Hydraulic System Cleanliness?
 
“Cleanliness” is a term used to describe the level of solid and
liquid contamination found in hydraulic systems. “Contamination”
is defined as any substance that is not part of the hydraulic system’s
working fluid.

Why is cleanliness important to your customers?

There are several reasons:
 
   Efficient production - clean systems provide for maximum productivity.

   Improved control  -  spare parts use can be controlled through preventive maintenance and monitoring  contamination.

   Reduce equipment downtime  - through scheduled inspections

   Safety hazards minimized - through preventing contamination related
failure for increased life expectancy of components on equipment.

Reduced repair cost  - due to fewer breakdowns.

 
Several reputable sources have claimed that 70 to 80 percent of
hydraulic system failures are due to contamination. By establishing
a contamination control program, costly repairs and downtime may
be minimized. A contamination  control program can be as simple
as establishing an allowable level of contamination within a hydraulic
system, supplying cleaned components for the system, and monitoring
levels of contamination as part of a preventive maintenance
program.


Search This Blog